
High temperature test equipment, such as environmental chambers, ovens, and furnaces, plays a critical role in material testing, product reliability validation, and accelerated aging studies. However, these systems are among the most energy-intensive assets in a laboratory or manufacturing facility. With rising electricity costs and tightening environmental regulations, optimizing energy efficiency has become a strategic priority for operations managers and procurement professionals. This guide provides a technical yet practical overview of how energy efficiency is measured, why it directly impacts your operating budget, and what specific technologies and design choices can significantly reduce power consumption without compromising test performance or safety.
Understanding Energy Efficiency in High Temperature Test Equipment
Energy efficiency in the context of high temperature test equipment refers to the ratio of useful thermal energy delivered to the test specimen relative to the total electrical energy consumed by the unit. The primary loss mechanisms include heat dissipation through chamber walls, air exchange during door openings, inefficiencies in heating elements, and standby power consumption. Key performance indicators (KPIs) to evaluate efficiency include:
- Heat-up rate – faster ramp times reduce the duration of high power draw but may require more powerful heaters, creating a trade-off.
- Thermal insulation quality – measured by the thermal conductivity (k-value) of insulation materials and thickness.
- Standby power consumption – the power drawn when the chamber is idle but maintaining setpoint temperature.
- Temperature uniformity – efficient systems maintain tight distribution with minimal energy input because airflow and heater placement are optimized.
- Recovery time after door opening – shorter recovery implies better insulation and heater control.
Why Energy Efficiency Matters for Your Bottom Line
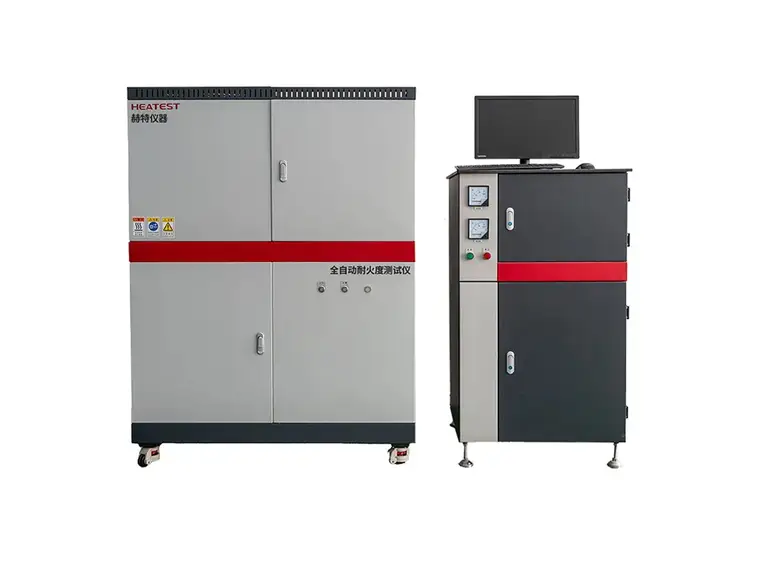
Choosing energy-inefficient equipment creates hidden costs that compound over the system’s 10–15 year lifespan. A typical 1000-liter high temperature chamber rated at 12 kW running 8 hours per day, 5 days per week, can consume over 20,000 kWh annually. At an average industrial electricity rate of $0.12/kWh, that translates to $2,400 per year for a single unit. A 20% improvement in efficiency saves $480 annually – and across a fleet of 10 units, the savings exceed $4,800 per year. Beyond direct cost, energy efficiency contributes to:
- Reduced HVAC load – less waste heat rejected into the lab lowers air conditioning costs.
- Compliance with sustainability mandates – many corporations and governments now require energy star ratings or ISO 50001 alignment.
- Improved equipment reliability – lower thermal stress on components extends service intervals.
Key Technologies Driving Energy Savings
Advanced Insulation Materials
Modern chambers use vacuum-insulated panels (VIPs) or microporous silica insulation with k-values as low as 0.004 W/m·K, compared to 0.035–0.045 for traditional mineral wool. This reduces heat loss by up to 60% at temperatures above 300°C. For example, HEATEST Instrument incorporates multi-layer ceramic fiber insulation in its HEAT-3000 series, achieving less than 2°C temperature drop over 8 hours in standby mode.
…
For more detailed information regarding energy efficiency guidelines for high-temperature test equipment, please click here: https://www.lyheatest.com/tester-knowledge/energy-efficiency-guide/

